Products / Sand reclamation
Sand reclamation · S1 to S4
From black sand back to white
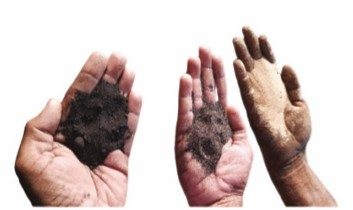
Green sand is expensive to buy and costly to dump. Rhino’s reclamation range recovers silica sand from used moulds and puts it back into the mould and the core.
Rhino research puts the sand foundries dispose of in India at about 12 million tonnes a year. Cold box cores made from 100% reclaimed sand have run at 0.65% binder with an ADV below 3.
The range
Four ways to reclaim sand
| Model | Method | Result |
|---|---|---|
| S1 | Mechanical | 75 to 85% of the sand recovered; models from 0.8 to 10 t/hr |
| S2 (S2C-Acidic, S2C-Basic) | Thermal, at 550 °C for chemically bonded and up to 750 °C for green sand. S2C-Acidic suits furan and phenolic binders; S2C-Basic suits alkaline binders, with research continuing | Uses 20 to 30% less gas |
| S3 | Mechanical, thermal, then mechanical | 80 to 85% recovered, for cold box, hot box and shell core sand; demonstrated in 2018 |
| S4 | Thermal after mechanical | Up to 90% of new sand replaced |
The older CO₂ sand reclamation range (RSM-50, RSM-150C continuous and RG-200 dry attrition) continues to serve silicate and CO₂ foundries.
Proven in foundries
Reference plants
Reference plants include Aqua Sub (2015 and 2020), CRI Pump (2016), Brakes India and its group companies (Flometallics 2017–18, Dunes in Oman 2023 and Sholingur 2025, a repeat customer in India and Oman), Magna Electrocasting (2020) and PSG Sons (2022). See the full list.
Rhino holds a patent for CO₂ sand reclamation (2000) and has worked with FATA, Italy, on green and thermal reclamation since 2013.
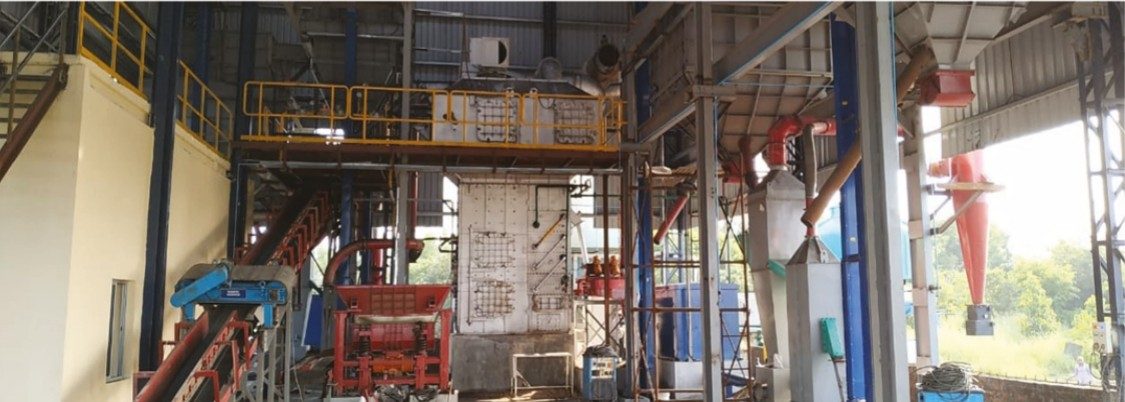
Pilot plant, Anand
A demonstration centre for foundry clusters
Rhino’s pilot plant at Anand is a demonstration centre for a common facility serving a cluster of foundries. It handles 1,000 kg an hour of green sand for moulding, 2,500 kg an hour of thermal regeneration and 2,000 kg an hour of green sand to core sand, on 540 m² of floor and 300 m² under cover with 350 HP installed. The first sand was reclaimed there on 20 December 2017, and pilots have run in three foundries.
Pilot results so far: about half the new sand bought, better surface finish with fewer rejections, and lower emissions. Rhino reports sand cost reductions of up to 70%. The next step is a cluster or common facility model.
Sustainable Development Goals
Where reclamation contributes
A detailed SDG impact note for sand reclamation is being prepared. Figures are indicative.
Gallery
Sand reclamation photo gallery


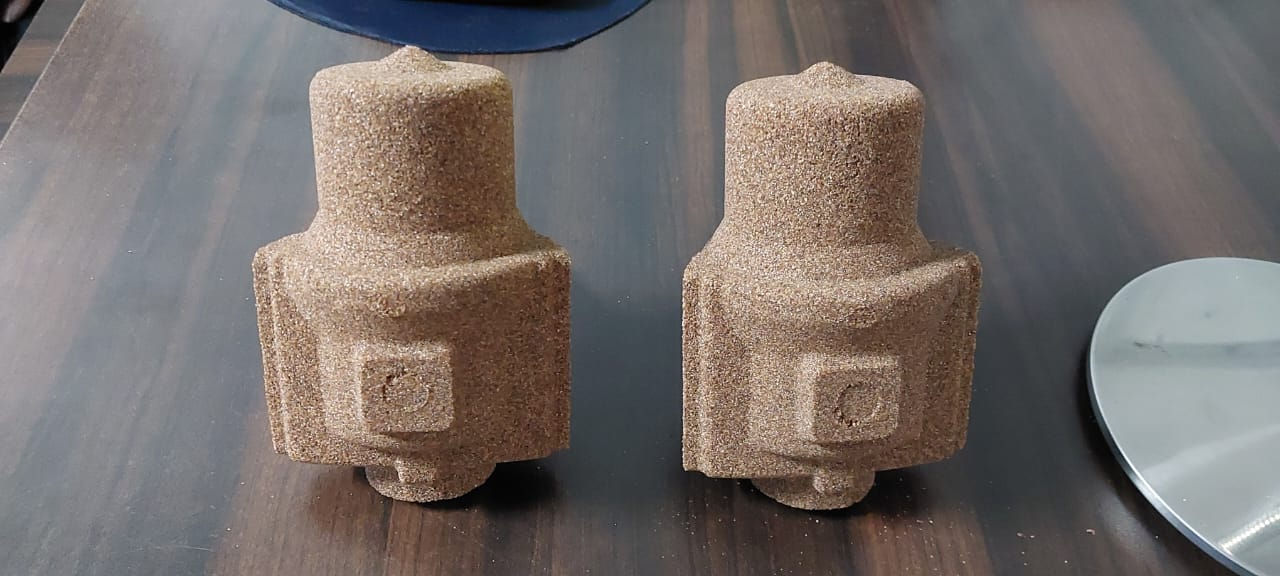

Select a photo to enlarge it.
Rajnikant Paghadar, SPB and Sand Reclamation Technologies
+91 95379 71060
Krutik Mevada, Sand Reclamation Process & Operations Support
+91 92271 20171